Sealing Machines / Induction Sealing Machines
Induction Cap Sealing Machine
Automatic air-cooled online induction cap sealing machine with non-contact electromagnetic foil heating, adjustable sealing head, PLC-HMI controls and three production configurations.
ISO 9001:2015Ahmedabad, IndiaManufacturer - Exporter
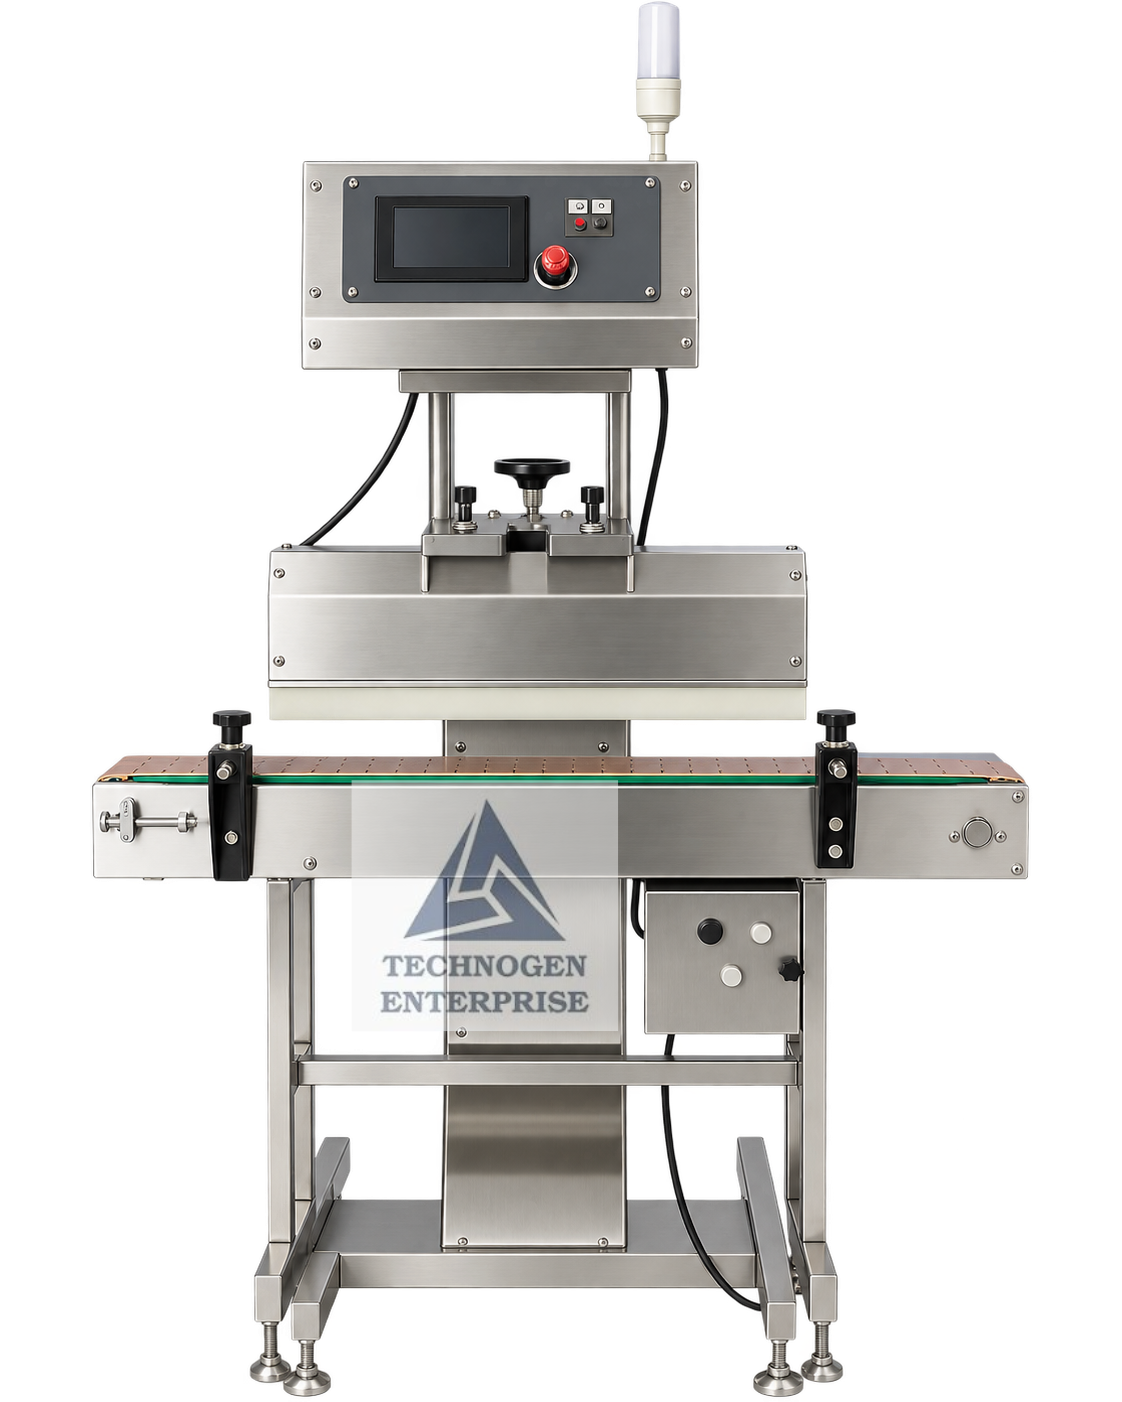
Induction Cap Sealing MachineMachine image shown for reference. Final configuration is selected against the approved application and production requirement.
01
Machine Overview
The Induction Cap Sealing Machine manufactured by Technogen Enterprise is an automatic, air-cooled packaging system designed to seal compatible foil induction liners onto bottle mouths through a non-contact electromagnetic heating process. Installed after the bottle capping machine, the equipment forms an important sealing stage in packaging operations where an additional tamper-evident barrier and protection against leakage or external contamination are required.
The machine is designed for continuous online production, with capped bottles moving beneath the induction sealing head on a conveyor. High-frequency electromagnetic energy interacts with the aluminium foil component of the induction liner, generating localized heat. Where the liner and bottle finish are compatible, this heat activates the heat-seal layer, allowing it to bond to the bottle mouth under the conditions established by the closure assembly and process settings.
The equipment is available in low-, medium- and high-speed configurations, with specified working ranges of 10–40, 10–60 and 10–90 bottles per minute respectively. Actual production output depends on bottle-neck diameter, liner design, available induction power, conveyor speed and sealing requirements.
The machine supports bottle-neck diameter groups of 20–60 mm and 60–100 mm and offers tunnel-type and broad-type induction sealing heads. Head selection should be matched to the container geometry and foil liner characteristics. The sealing head height can be adjusted over the specified 0–300 mm range to suit the container passing through the sealing station.
The air-cooled induction system incorporates a condenser, output transformer and cooling fan within the specified induction head arrangement. This construction provides the machine's cooling method without the need to describe it as a water-cooled sealing system. The machine body is manufactured using AISI 304 stainless steel in a compact, cGMP-oriented design.
A PLC-HMI operator interface provides access to machine operating functions, while the current controller, adjustable voltage protector and sealing-time controls support adjustment of induction heating conditions. The operating panel includes main power, start and stop controls, conveyor switching and speed adjustment. A variable frequency drive provides conveyor speed variation.
With three available production configurations and adjustable induction sealing heads, the machine can be integrated into appropriate pharmaceutical, food, beverage, cosmetic and chemical bottle packaging lines after suitable liner compatibility testing.
Technogen Enterprise, headquartered in Ahmedabad, Gujarat, India, is a manufacturer, supplier and exporter of induction cap sealing machinery for domestic and international packaging applications requiring controlled electromagnetic foil liner sealing.
02
Applications
03
Operating Principle
The machine operates on the electromagnetic induction sealing principle, in which appropriately capped bottles pass beneath a powered induction head and the aluminium component of the liner is heated without direct contact between the sealing head and the closure.
Bottle and Liner Preparation
The bottle is fitted with a cap containing a suitable induction sealing liner. The liner structure, closure and bottle-neck finish must be compatible with induction sealing.
Bottle Infeed
The capped bottles arrive from the upstream capping operation and travel on the machine conveyor toward the induction sealing station.
Sealing Head Positioning
The induction sealing head is adjusted to the appropriate height above the bottle cap. Tunnel-type or broad-type head selection is established according to bottle and liner requirements.
Electromagnetic Heating
As the capped bottle passes beneath the energized induction head, electromagnetic energy generates heat within the aluminium foil component of the induction liner.
Heat-Seal Layer Activation
The heat generated in the foil activates the liner's heat-sealing layer. With suitable cap application conditions, the liner bonds to the bottle-neck sealing surface.
Cooling and Seal Formation
Following induction exposure, the liner and bottle assembly cool. Seal integrity depends on the combination of liner compatibility, induction energy, conveyor speed and bottle closure conditions.
Power and Speed Adjustment
The current controller, PLC-HMI and speed controls are used to establish suitable sealing settings for the bottle and liner combination.
Bottle Discharge
Processed bottles leave the induction sealing station for downstream inspection, labeling or other packaging operations.
04
Salient Features
Automatic air-cooled online induction cap sealing machine
Non-contact electromagnetic induction heating principle
Suitable for integration after an automatic bottle capping machine
Three low medium and high-speed configurations
Specified production capacities up to 40 60 and 90 bottles per minute
AISI 304 stainless steel machine construction
Compact cGMP-oriented machine layout
Tunnel-type induction sealing head configuration
Broad-type induction sealing head configuration
Compatible neck diameter groups from 20 mm to 60 mm and 60 mm to 100 mm
Adjustable induction sealing head height from 0 mm to 300 mm
Air-cooled induction head with condenser output transformer and cooling fan
Inbuilt programmable logic controller and human-machine interface
Current controller for induction power adjustment
Adjustable voltage protector
Adjustable heating time to match production requirements
Variable frequency drive for conveyor speed adjustment
Operating panel with main power on-off control
Start and stop push buttons for machine operation
Conveyor on-off switching and speed adjustment
Designed for continuous processing of correctly capped bottles with compatible foil liners
05
Technical Specifications
Final specifications may vary with container size, product characteristics, selected model and approved configuration.
| Parameter | TGAICS-50BR | TGAICS-80BR | TGAICS-100BR |
|---|---|---|---|
| Machine Speed | 10 to 40 bottles/minute depending on bottle-neck diameter | 10 to 60 bottles/minute depending on bottle-neck diameter | 10 to 90 bottles/minute depending on bottle-neck diameter |
| Neck Diameters | 20–60 mm and 60–100 mm | 20–60 mm and 60–100 mm | 20–60 mm and 60–100 mm |
| Type of Head | Tunnel Type and Broad Type Head | Tunnel Type and Broad Type Head | Tunnel Type and Broad Type Head |
| Sealing Method | Non-contact electromagnetic heating process | Non-contact electromagnetic heating process | Non-contact electromagnetic heating process |
| Adjustable Height of Sealing Head | 0–300 mm | 0–300 mm | 0–300 mm |
| Power Consumption | 1 kW | 2 kW | 2.5 kW |
| Electrical Connection | 230 V AC, Single Phase, 50 Hz | 230 V AC, Single Phase, 50 Hz | 230 V AC, Single Phase, 50 Hz |
| Induction Sealing Unit Footprint (L × W × H) | 800 × 800 × 1500 mm | 900 × 900 × 1500 mm | 950 × 950 × 1500 mm |
| Conveyor Length | 1530 mm | 1830 mm | 2130 mm |
06
Machine Interlocks & Safety Features
Adjustable voltage protector for electrical supply protection
Current controller for setting induction heating conditions
Cooling fan integrated into the air-cooled induction sealing assembly
07
Applicable Industries
08
Frequently Asked Questions
What is an Induction Cap Sealing Machine?
It is a machine that uses electromagnetic induction to heat compatible foil liners inside bottle closures so the liner can bond to the bottle mouth and form a tamper-evident seal.
Where is the induction sealer installed in a packaging line?
The automatic air-cooled machine is designed for installation after the bottle capping operation, allowing capped bottles to pass beneath its induction sealing head.
What production speeds are available?
Three configurations are specified, covering 10–40, 10–60 and 10–90 bottles per minute depending on the bottle-neck diameter and selected operating conditions.
What bottle-neck sizes can the machine handle?
The specifications provide two neck-diameter groups: 20–60 mm and 60–100 mm. Head selection and bottle compatibility must be established for the application.
What is the difference between a tunnel head and a broad head?
They are different induction head arrangements intended for suitable container and liner geometries. The correct head should be chosen after evaluating the bottle, cap, foil liner and required sealing conditions.
Does induction sealing require contact between the machine head and the cap?
No. Electromagnetic induction sealing is a non-contact heating process, although the foil liner must be correctly positioned and supported by the closure assembly.
Is the induction sealing machine air-cooled?
Yes. The machine is specifically described as air-cooled and incorporates a cooling fan in its induction head arrangement.
Does induction sealing guarantee leak-proof packaging?
Seal quality depends on liner construction, bottle-neck condition, closure application and validated induction settings. Packaging performance should be established through suitable seal testing.
Product Updates
Latest updates for Induction Cap Sealing Machine.
Kenya
Induction Cap Sealing Machine Supplier in Kenya
Technogen Enterprise supports manufacturers with induction cap sealing machinery for leak protection, tamper evidence and dependable bottle-mouth s...
Read UpdateRelated Machinery
Continue building your line.
Aluminium Foil Sealing Machines
Automatic 4 Head Bottle Aluminum Foil Sealing Machine
Automatic four-head aluminium foil conduction sealing machine with foil roll feeding, synchronized bottle handling, PLC and 7-inch HMI, digital temperature control and No Bottle–No Foil operation.
Aluminium Foil Sealing Machines
Automatic Bottle Aluminum Foil Sealing Machine
Automatic single-head aluminium foil sealing machine with heat-conduction sealing, foil roll feeding, cutting, precise temperature control, PLC-HMI and No Bottle–No Foil operation.
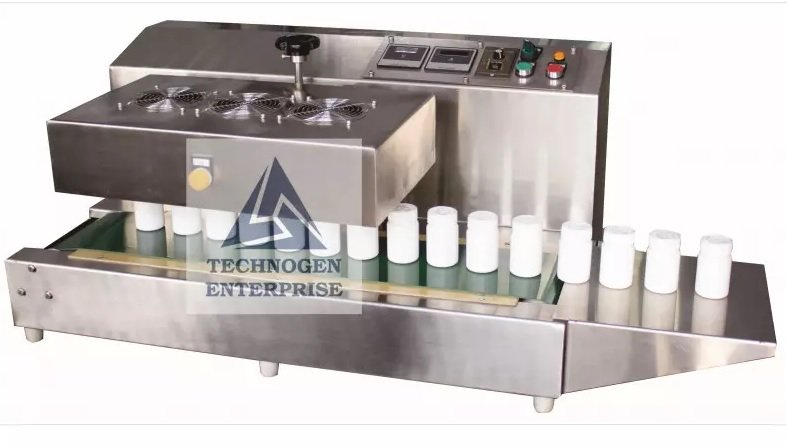
Induction Sealing Machines
Automatic Portable Induction Sealing Machine
Compact automatic portable induction sealer with integrated conveyor, air-cooled electromagnetic sealing head, adjustable heating controls and output from 20 to 40 bottles per minute.
Request Technical Quote
Discuss Induction Cap Sealing Machine with our engineering team.
Share your bottle-neck diameter, bottle height, cap design, induction foil liner specification, required output and packaging-line arrangement with Technogen Enterprise for selection of the appropriate induction sealing head and machine configuration.